Precision EDM for deep, narrow apertures
Precision Small Hole EDM Services
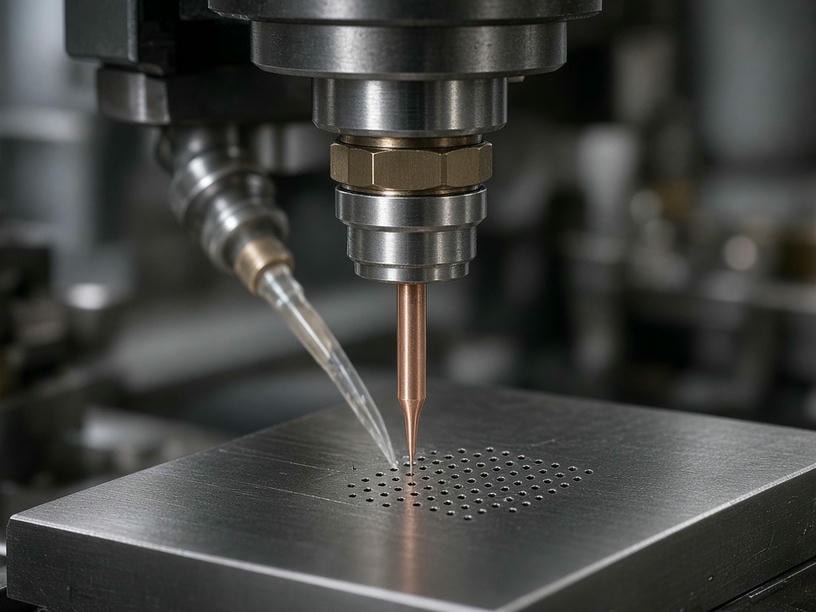
PartsMake specializes in small hole electrical discharge machining for components that require deep, narrow, or high-precision apertures. Our process supports hardened parts, conductive superalloys, and geometries that are difficult to reach with conventional drilling.
Technical capability
Small hole EDM parameters built for demanding parts
High-frequency electrode rotation and specialized dielectric flushing help maintain geometric integrity when traditional drilling could cause tool deflection or breakage.
Typical engineering focus
Up to 50:1
Maximum depth-to-diameter ratio, material dependent
| Specification | PartsMake Capability |
|---|---|
| Hole diameter range | Ø0.3 mm – Ø3.0 mm |
| Maximum depth-to-diameter ratio | Up to 50:1, material dependent |
| Positional tolerance | Down to ±0.01 mm |
| Electrode materials | Brass or copper, solid or hollow |
| Electrode diameter | Selected to suit the specified hole diameter and material |
| Workpiece materials | Inconel, titanium, hardened steel, tool steel, carbide |
| Workpiece thickness / size | Maximum workpiece envelope: 500 × 400 × 300 mm |
Process control
Control for high-aspect-ratio holes
Deep-hole accuracy depends on rigorous control over electrode wear and spark-gap stability. We manage these variables to reduce wandering and taper in holes with demanding depth-to-diameter ratios.
01
Stable spark gap
Controlled EDM conditions support consistent internal geometry through narrow and deep apertures.
02
Reduced wandering
Electrode rotation and specialized dielectric flushing help maintain hole location and direction.
03
Material versatility
The process is suited to conductive superalloys, hardened steels, tool steels, titanium, and carbide.
Application coverage
Where small hole EDM adds value
From starter holes to internal cooling paths, the process integrates into demanding production workflows.
Turbine blades
Precision cooling holes in Inconel and nickel-based superalloys.
Mold and die tooling
Starter holes for wire EDM profiles and ejector pin clearances.
Nozzle orifices
Micro-nozzles and flow restrictors requiring defined surface integrity.
Medical and aerospace fixtures
Complex hardened components with tight-tolerance internal geometry.
Single-source manufacturing
Combine EDM with precision grinding
Many projects require EDM and secondary finishing to reach final dimensions. PartsMake combines EDM for internal features with precision cylindrical or surface grinding for external mating surfaces.
This single-source approach helps reduce lead times and supports consistent transitions between EDM-machined holes and ground surfaces on stringent engineering drawings.
Facility equipment capabilities
- ●Wire EDM: Profile cutting with tolerances down to ±0.005 mm.
- ●Sinker EDM: Complex cavity and internal geometry machining.
- ●Cylindrical grinding: Capacity up to Ø300 × 1000 mm.
- ●Surface grinding: Precision finishing up to 600 × 300 mm.
Quality assurance
Inspection evidence for every batch
Every component follows a standardized verification process to support dimensional consistency, surface integrity, and material traceability.
Start an engineering review
Request a small hole EDM quote
Send your technical drawings in PDF or STEP format, material specifications, and volume requirements for an accurate assessment.
Address
Talk with our engineering team
Share your requirements and receive guidance on hole diameter, depth, material, and inspection needs.