Custom sheet metal fabrication
Custom Sheet Metal Welding Services
Build complex sheet metal assemblies with controlled heat input, repeatable positioning, and weld integrity engineered around your product requirements.
PartsMake supports prototypes through high-volume production for enclosures, chassis, frames, and structural components, with welding coordinated alongside cutting, bending, and finishing.
4
Core welding processes
1
Integrated fabrication partner
Process selection
The right weld starts with the right process
Our engineering team reviews your CAD files, material, sheet thickness, joint design, appearance requirements, and production volume before recommending the most efficient welding strategy.
TIG Welding
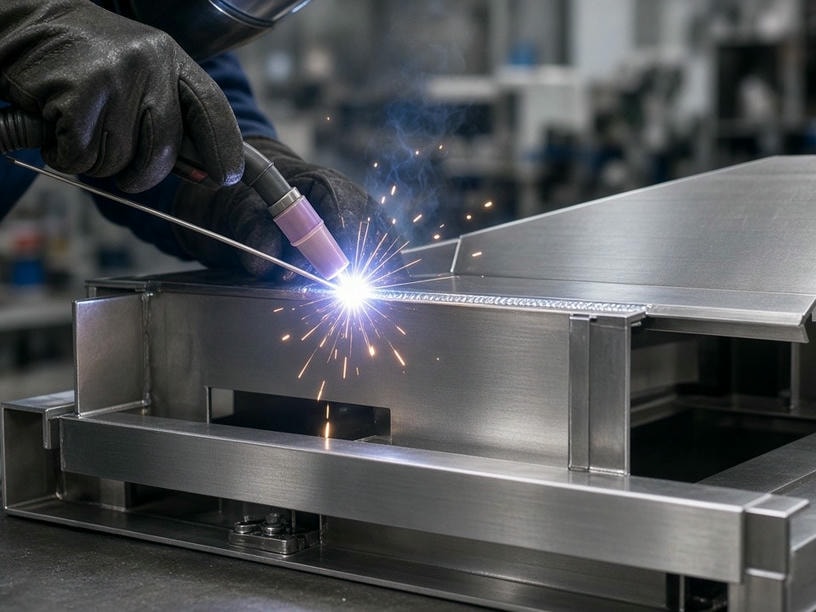
High control over the arc and filler material for thin-gauge stainless steel and aluminum enclosures where a clean, aesthetically pleasing seam matters.
MIG Welding
High deposition rates and strong penetration for structural frames, heavier-gauge steel, industrial brackets, and machinery frames.
Laser Welding
A narrow, deep weld with very low heat input and minimal post-processing for medical devices, precision electronics housings, and tight-tolerance assemblies.
Spot Welding
A rapid, reliable solution for overlapping sheets in cabinets, panels, and internal structural components where exposed fasteners are not required.
Engineering comparison
Compare heat, penetration, finish, and speed
Use the process profile below as a starting point. The final recommendation depends on your joint geometry, material, thickness, tolerances, and production volume.
| Process | Heat input | Penetration | Finish quality | Speed | Best for |
|---|---|---|---|---|---|
| TIG | Low / Medium | Moderate | High, cosmetic | Slow | Thin-gauge, precise joints |
| MIG | High | Deep | Moderate | Fast | Structural, thicker materials |
| Laser | Very low | Very deep | Excellent | Very fast | High-precision, low-distortion parts |
| Spot | Localized | Not applicable | Functional | Fast | High-volume sheet overlap |
Quality by design
Control distortion before it becomes a production problem
Welding introduces thermal stress that can cause warping, dimensional inaccuracies, and rejected parts. PartsMake uses engineering-led preparation to stabilize assemblies from prototype through repeat production.
Send your drawings for reviewFixturing and positioning
Custom welding fixtures hold components in a rigid structure, counteracting thermal expansion and contraction while protecting dimensional tolerances.
Documented weld sequencing
Alternating weld locations and managing cooling rates distributes heat across the part to reduce pulling, twisting, and localized distortion.
03
Post-weld processing
- Grinding & blendingRemove spatter and blend beads to match the base material profile.
- Surface preparationDeburr and clean surfaces for powder coating or anodizing adhesion.
- VerificationInspect dimensions so assemblies fit mating hardware and enclosures.
Application guidance
Match the weld to the finished product
Selecting the process early reduces cost, post-processing, and quality risk across the production lifecycle.
Cosmetic assemblies
For visible enclosures and customer-facing surfaces, TIG or Laser welding creates cleaner seams that can be blended during finishing.
High-strength structures
For frames, load-bearing brackets, and heavier-gauge components, MIG welding provides penetration and speed while controlling labor cost.
Tight tolerances and seals
For mating parts or air-tight assemblies, Laser or TIG welding helps minimize the heat-affected zone and reduce deformation risk.
Specification support
Built for cosmetic and mechanical requirements
Our team can review your drawings and recommend welding, finishing, and inspection details for the final application.
Air-tight requirements: prioritize controlled heat input and appropriate TIG or Laser weld strategies.
Visible surfaces: define blend, bead, spatter, and surface preparation expectations before production.
Repeat production: use dedicated fixtures and documented weld sequences for unit-to-unit consistency.
Common project inputs
Files
STEP, IGES, or DXF files plus 2D drawings
Materials
Alloy, grade, sheet thickness, and finish
Quality
Tolerances, appearance, sealing, and inspection needs
Volume
Prototype quantity or repeat production demand
From prototype to production
A single-source partner for welded sheet metal assemblies
We integrate welding with laser cutting, bending, and finishing so your assembly moves through one coordinated manufacturing workflow.
-
1
Submit your CAD files
Send STEP, IGES, or DXF files and 2D drawings.
-
2
Specify your requirements
Include material, tolerances, welding expectations, and finishing such as powder coating or anodizing.
-
3
Receive an engineering review
Get a DFM review and competitive quote based on your design and volume.
Welding questions
Plan your next welded assembly
Start your project
Ready to move your welded assembly into production?
Send your CAD files and requirements to PartsMake. Our engineering team will review the design and suggest the right welding strategy.
Email:
Facility:
Request a quote
Include drawings, material, thickness, tolerances, finish, and estimated quantity.