Precision Cylindrical Grinding Services
PartsMake specializes in high-precision cylindrical grinding for components requiring strict geometric control. We support shafts, pins, and rotary components that demand accurate bearing fits, seal diameters, and superior surface integrity on hardened alloys.
±0.002 mm
Dimensional tolerance
Ra 0.2 μm
Surface finish capability
Ø300 mm
Maximum diameter
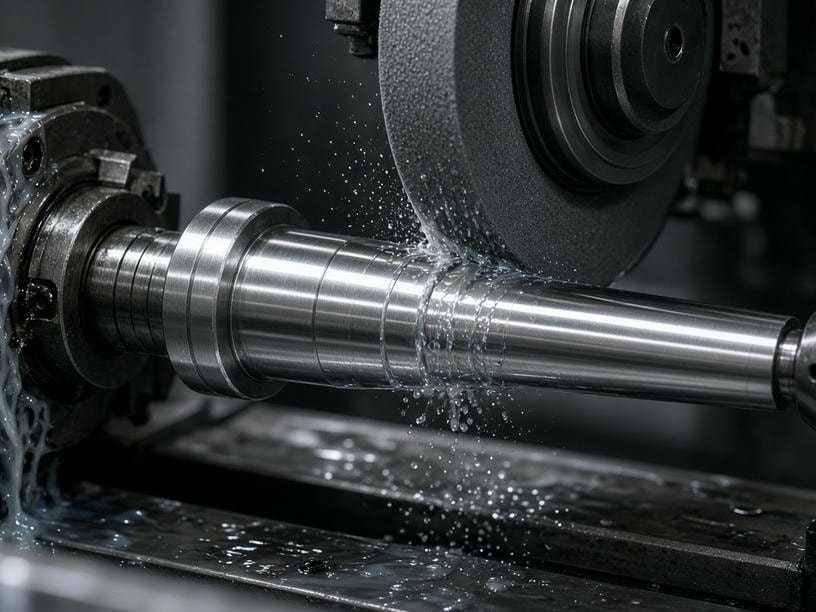
Built around the print
Center-hole references, grinding allowance, bearing fits, and seal positions are reviewed before production.
Technical specifications
Controlled geometry for demanding assemblies
Our grinding capabilities are calibrated for tight-tolerance production. We maintain rigorous control of roundness, cylindricity, and coaxiality to support high-speed and high-load mechanical assemblies.
Typical application focus
- OD and ID finishing for shafts, journals, pins, and rotary components
- Center-hole-based setups for accurate alignment to the central axis
- Hardened alloys requiring controlled stock removal after heat treatment
| Specification | Capability / review basis |
|---|---|
| Maximum diameter | Up to Ø300 mm |
| Maximum length | Up to 1000 mm |
| OD / ID range | OD and ID features reviewed against drawing, tooling, and workholding requirements |
| Dimensional tolerance | Down to ±0.002 mm |
| Roundness | Controlled to the engineering drawing requirement |
| Cylindricity / coaxiality | Verified as critical geometric controls for mating assemblies |
| Surface finish | Down to Ra 0.2 μm |
| Materials | Steel, stainless steel, tool steel, and hardened alloys |
Functional surfaces
Optimized for shaft and bearing mating surfaces
Cylindrical grinding is the final step in producing functional shafts. We focus on the surface and geometric parameters that define long-term component reliability.
Bearing fits
Precision grinding achieves the specified interference or clearance fits required for high-speed rotation.
Seal diameters
Surface finishes down to Ra 0.2 μm help prevent premature seal wear and fluid leakage.
Geometric control
Roundness and cylindricity control helps minimize vibration and runout in mechanical assemblies.
Hardened components
Heat-treated shafts can be ground after tempering to correct distortion while preserving the required geometry.
Process integration
From CNC machining to finish grinding
While PartsMake offers standalone grinding services, we frequently integrate grinding with CNC machining. Rough turning and heat treatment are typically completed before the final precision grind.
Prepare the datum
Center holes and reference features establish the axis for consistent support and alignment.
Account for distortion
The process sequence considers heat-treatment movement and the required post-treatment grinding allowance.
Finish functional surfaces
Mounting surfaces, journals, seal positions, and keyways are aligned to the central axis.
Engineering guidance
Plan the grinding allowance early
Selecting the correct grinding allowance is critical for cost-effective production. We recommend leaving sufficient material after heat treatment—typically 0.1 mm to 0.3 mm depending on part geometry and material—so distortion can be removed while achieving the final finish.
Discuss your tolerance stack-upQuality control
Measurement that supports your drawing
Every component processed at PartsMake undergoes a documented inspection sequence. Calibrated measurement equipment is used to verify that parts meet the provided engineering drawings.
CMM
Verifies coaxiality and position.
Micrometers
Diameter verification to 0.001 mm resolution.
Roughness testers
Confirms Ra values for seals and bearings.
Standard documentation package
- ✓Dimensional inspection reports
- ✓Material certificates
- ✓Hardness verification
- ✓Full batch traceability for production runs
Application flexibility
Grinding and EDM in one production strategy
For components requiring more than external grinding, cylindrical grinding can be combined with internal EDM services to complete hardened and complex features without compromising the finished geometry.
Hardened steel dies
Grind the outer diameter while using sinker EDM for internal cavities.
Complex shafts
Use wire EDM to create keyways or intricate profiles on ground shafts without inducing mechanical stress.
Small hole features
Add lubrication holes or internal channels to hardened shafts with precision EDM.
Common project considerations
Built for critical shaft features
Ready for review
Let our engineers review your print
If you are finalizing a design or need support with tolerance stack-ups for mating components, our engineering team can review your drawings and suggest an efficient machining sequence.
Start a Technical DiscussionRequest a quote
Send your cylindrical grinding requirements
To receive a formal quote, please send your technical drawings in PDF or STEP format. Include material requirements, required tolerances, and expected batch quantities.